
Key Points to Ensure Lead Content in Mosquito Swatter Solder Joints Meets Standards
2025-09-28
Key Points to Ensure Lead Content in Mosquito Swatter Solder Joints Meets Standards!
Recently, some customers have raised the requirement that the lead content in the solder joints of mosquito swatters must not exceed the standard when consulting and placing orders.
In the production process of mosquito swatters, whether the lead content in solder joints meets the standard carries significant importance: it not only determines whether the product complies with national environmental protection standards (e.g., the lead content restrictions in the RoHS Directive) but also directly impacts consumers' health and the ecological environment. Unfortunately, many enterprises often neglect key links during production, leading to excessive lead content in solder joints and subsequent risks such as product recalls and blocked market access. This article will detail the core measures to solve this problem.
1. Source Control: Selecting the Right Low-Lead / Lead-Free Soldering Materials
The "root cause" of excessive lead content in solder joints often lies in raw materials. Therefore, selecting and managing soldering materials properly is the first line of defense to avoid excessive lead.
1.1 Prioritize Lead-Free Soldering Materials with Qualified Certifications
Compliant lead-free solder is typically tin-based, mixed with elements like silver, copper, and zinc, and its lead content must be strictly controlled below 1000ppm (0.1%). When purchasing:
- Require suppliers to provide authoritative test reports (e.g., SGS, CTI certificates) to confirm that lead content meets national standards such as GB/T 20422-2006.
- Avoid choosing low-cost, uncertified solder, as such products often have hidden lead content risks.
1.2 Strictly Separate Lead-Containing and Lead-Free Materials
- Set up independent storage areas for lead-free materials in the workshop, with clear labels (e.g., "Lead-Free Solder Storage Area") to prevent mixing.
- Train warehouse staff to check material labels twice before issuing goods, ensuring that lead-free materials are not mistakenly replaced with lead-containing ones. A painful lesson: an enterprise once placed lead-containing and lead-free solder wires on the same shelf, resulting in excessive lead content in an entire batch of products.
2. Process Optimization: Standardizing Soldering Operations and Parameters
High-quality lead-free materials can only play their role if matched with scientific soldering processes. Optimizing process parameters and standardizing operations are key to preventing lead enrichment in solder joints.
2.1 Adjust Soldering Equipment Parameters to Match Lead-Free Solder
The melting point of lead-free solder is higher than that of lead-containing solder (e.g., the melting point of Sn-Ag-Cu lead-free solder is about 217℃, while that of lead-containing solder is about 183℃). Improper temperature settings will affect solder joint quality and lead content stability:
- Set the electric soldering iron temperature between 280-320℃, and adjust it according to the specific model of lead-free solder (refer to the supplier's recommended parameters).
- Control the soldering time within 1-3 seconds: too short a time leads to cold soldering, while too long a time causes solder oxidation and possible lead element aggregation.
2.2 Standardize Employee Soldering Operating Procedures
Unstandardized operations are another major cause of excessive lead content. Enterprises should formulate clear operating guidelines:
- Before soldering: Clean the soldering iron tip with a cleaning sponge to remove residual solder and impurities (old lead-containing solder residues may contaminate new lead-free solder).
- During soldering: Keep the electric soldering iron in vertical contact with the solder joint, and complete the soldering in one go. Avoid repeated soldering, as it easily causes lead element enrichment in the solder joint and increases the risk of exceeding the standard.
3. Testing and Supervision: Controlling Lead Content Risks Throughout the Whole Process
"Post-event rectification" is far less effective than "full-process prevention". Establishing a multi-link testing system can timely detect lead content risks and avoid large-scale losses.
3.1 Incoming Inspection: Block Unqualified Materials at the Warehouse Gate
For each batch of incoming solder wire/solder paste:
- Randomly sample 3-5 pieces, and use an X-ray fluorescence spectrometer (XRF) to test the lead content. Only materials that meet the standard (lead content < 1000ppm) can be put into the warehouse.
- If the test result shows that the lead content is close to the standard upper limit (e.g., 800-900ppm), increase the sampling quantity to 10-15 pieces and conduct a re-test to confirm whether there is a batch quality problem.
3.2 In-Process Sampling: Monitor Solder Joint Quality in Real Time
During production:
- For every 100 mosquito swatters produced, randomly select 2-3 units for solder joint disassembly. Focus on testing key solder joints (e.g., the connection between the power grid and wires, the connection between the switch and circuit board).
- If excessive lead content is found in any solder joint, immediately suspend production, and investigate the cause (whether it is due to material replacement, parameter deviation, or operational errors) before resuming production.
3.3 Finished Product Inspection: Ensure 100% Compliance Before Delivery
Before the mosquito swatters leave the factory:
- Use a portable XRF detector to conduct rapid lead content screening on the solder joints of each product, ensuring no unqualified products flow into the market.
- Keep all test records (incoming inspection, in-process sampling, finished product inspection) for at least 2 years, so that if quality problems occur later, the cause can be traced quickly.
4. Personnel Management: Enhancing the Environmental Protection and Quality Awareness of All Employees
Employees are the executors of production processes. Improving their awareness of lead-free soldering and operational skills is the guarantee for the implementation of all measures.
4.1 Conduct Regular Training on Lead-Free Soldering Knowledge
- Theoretical training: Explain the harm of lead (e.g., damage to the human nervous system and digestive system) and the consequences of excessive lead content (e.g., product recalls, brand reputation damage) to let employees understand the importance of lead control.
- Practical training: Demonstrate the use of lead-free solder, the adjustment of soldering iron temperature, and the standard soldering process. After training, organize practical assessments, and only employees who pass the assessment can take up their posts.
4.2 Establish a Reward and Punishment Mechanism to Strengthen Supervision
- Rewards: For employees who strictly abide by operating procedures and whose teams have no lead-exceeding products for 3 consecutive months, provide cash rewards or honorary certificates.
- Punishments: For employees who cause excessive lead content in products due to improper operations (e.g., using lead-containing solder by mistake, repeated soldering), arrange re-training; if the mistake is repeated, link it to performance evaluation (e.g., deduct performance points).
Conclusion
Ensuring that the lead content in mosquito swatter solder joints does not exceed the standard is not a "single-link task" but a "systematic project" that requires collaboration across raw material selection, process optimization, testing supervision, and personnel management.
Only by strictly controlling each link—eliminating lead risks from the source, standardizing operations in the process, and strengthening awareness in management—can enterprises truly produce products that comply with environmental protection standards and reassure consumers, thereby gaining a firm foothold in the competitive market.
Mosquito Traps Are Sensitive Skin & Allergy Sufferers' Best Defense
The Role of Water in Granular Insecticide Efficacy
Related Article
If you’re struggling with annoying mosquitoes, flies, and other flying pests indoors and outdoors, upgrading from traditional manual tools to anElectric Mosquito Swatter is the most efficient solution. Many homeowners and renters search where to buy fly swatter online to find durable, safe, and high-performance electric models that deliver instant pest control.
Where to Buy Fly Swatter
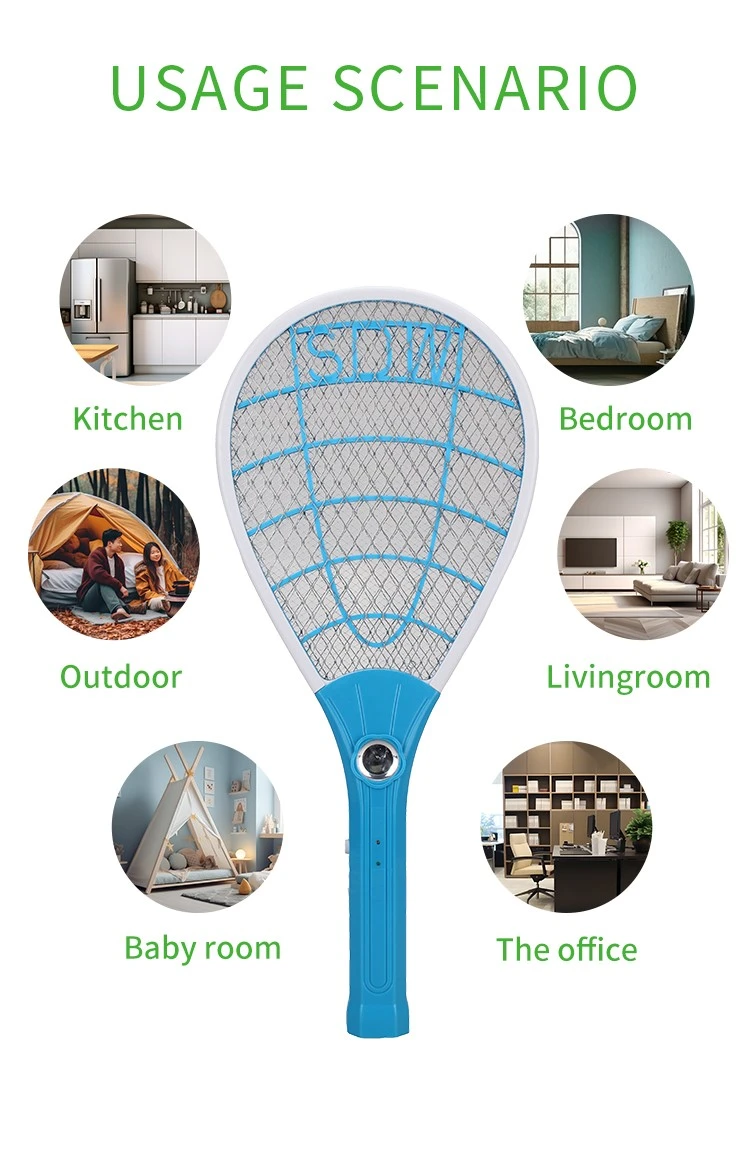
Most importers of electric mosquito swatters obsess over the first order: samples requested, factories vetted, a pre-shipment inspection booked. Then the reorder arrives eight months later and something is off. The grid feels softer. The charge port is a slightly different shade of black. The carton thickness dropped from 350 gsm to 300 gsm. Nothing is catastrophic — but the product no longer matches what your retail customers approved, and quietly, your return rate starts climbing.
How to Keep Mosquito Swatter Quality Consistent Across Repeat Orders
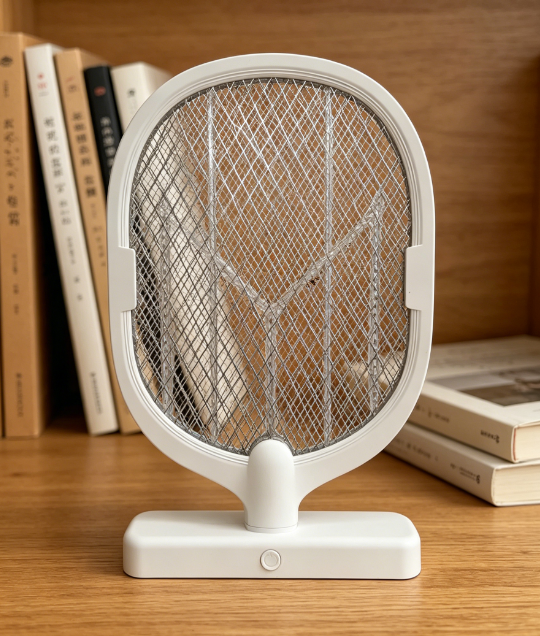
Warranty returns are the silent margin killer in the mosquito control category. A distributor who buys a swatter at $1.80 FOB and retails it at $9.90 can absorb a 1% return rate without noticing — but at 5%, the combined cost of replacement units, reverse logistics, and refund processing erases most of the line's profit.
Common mosquito swatter killer lamp failure modes wholesale spec guide
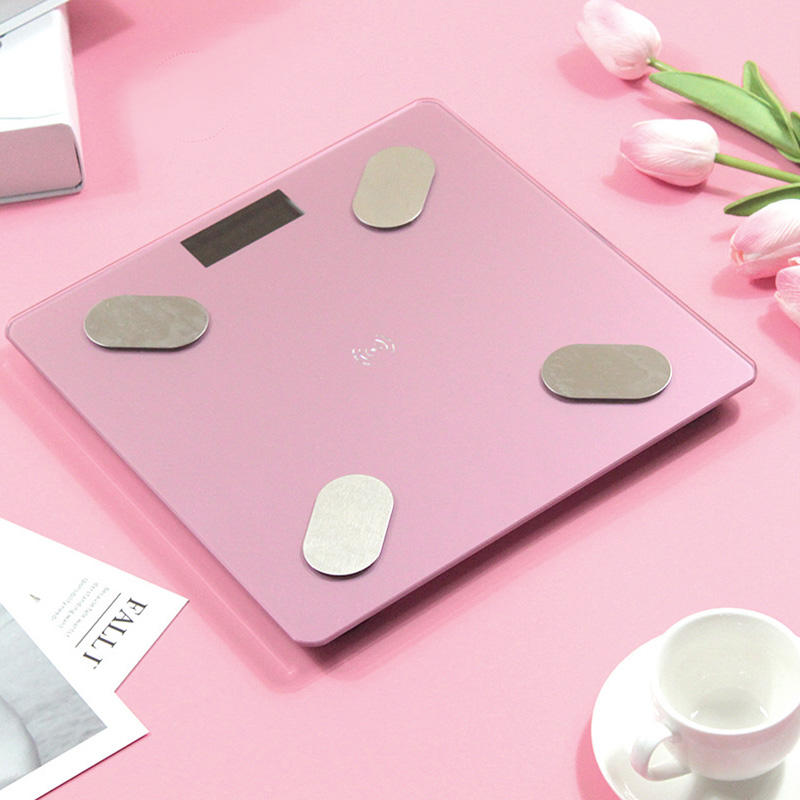
Digital bathroom scales rank as the second-highest-volume consumer weighing product category, only behind kitchen scales, with distinct market and product characteristics that set them apart from other scale types in importers’ product portfolios.
Digital bathroom body fat-bia-scale wholesale buyers guide